Products Features

High-Intensity Comprehensive Performance (Core Advantage)
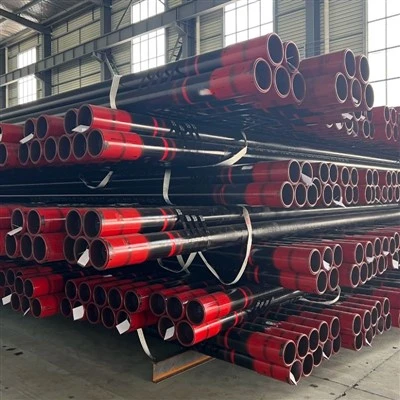
N80-1 Core Advantages: Normalized to obtain a ferrite-pearlite microstructure, it has higher strength than J55/K55, offers excellent cost-performance, and is commonly used for medium-deep wells and high-pressure non-sulfur oil and gas wells. It is also a frequently used oil casing steel grade for high-pressure sweet wells. Both seamless and ERW welded pipes are supplied as standard.
|
Performance indicators |
PSL1 Requirements |
|
Minimum Yield Strength (MPa) |
552 |
|
Maximum Yield Strength (MPa) |
758 |
|
Minimum Tensile Strength (MPa) |
- |
|
Yield strength ratio |
No mandatory requirements |
|
Elongation |
Calculate and determine using the tabular formula from API Spec 5CT |
Note: N80-1 Yield Range 552-758 MPa; higher strength than J55 and K55; lacks resistance to H₂S sulfide stress cracking and must not be used in sour wells; for H₂S service conditions, L80-1 or other anti-sulfur grade steels should be selected.

Good welding performance (core requirement for oil and casing pipes)
API 5CT N80-1 is heat-treated by normalizing, with controllable welding process, meeting the requirements for on-site construction and coupling welding. The carbon content of N80-1 is generally ≤0.43%, and the manganese content is controlled according to API specifications; it has a moderate risk of welding hardening, and its welding requirements are slightly higher than those of J55/K55 carbon steel.
Key Welding Points:
- Strictly implement WPS welding procedure qualification, control heat input, reduce the hardening tendency of the heat-affected zone, and minimize the risk of cold cracks.
- Strictly control harmful impurities P and S to ensure the purity of the base material and weld seam
- Supports seamless pipe butt welding, and also supports on-site ring welding of ERW welded pipes
Important Note: N80-1 is a high-strength carbon steel with strict welding process requirements. For thick-walled joints, preheating to 100-150°C is recommended. This is an engineering practice experience value; the API standard does not mandate a preheating temperature. Actual operations shall comply with the WPS (Welding Procedure Specification) welding procedure qualification. The base material itself does not have sulfide stress cracking resistance, and the weld is also not resistant to sulfur.

Good toughness and resistance to brittle fracture
N80 1 is only PSL1 grade. Under API standards, Charpy impact testing is not mandatory for PSL1; however, it is mandatory for PSL2 (after Annex H is activated). The base microstructure is ferrite-pearlite, which meets the requirements for service in medium-deep, high-pressure non-sulfur oil and gas wells at normal temperatures. For low-temperature severe service conditions, impact test requirements need to be agreed upon in the contract.
Typical impact requirements (to be implemented only if agreed in the contract or Annex H is activated):
- Test Temperature: According to the user's project requirements
- Impact energy: as agreed in the procurement agreement

Good corrosion resistance and environmental adaptability
API 5CT N80-1 is a general carbon steel casing pipe, which has uniform corrosion resistance in atmospheric, fresh water, soil, and dry oil and gas media without sulfur. It cannot be used in H₂S acidic oil and gas environments; for CO₂ corrosion conditions, corrosion rate assessment is required, and 13Cr corrosion-resistant alloy should be selected for severe corrosion environments.
Note: N80-1 is a conventional high-strength carbon steel, not a sour service steel; once the medium contains hydrogen sulfide, there is a risk of sulfide stress cracking failure.
Good cold bending and processing performance
API 5CT N80-1 is a normalized steel pipe. Cold bending requires control of deformation; hot bending can be used to manufacture elbows. The pipe ends support threading, upsetting, and beveling. They can be processed into STC/LTC/BTC and Premium special thread connections, meeting the API 5CT thread and coupling technical requirements.
Technical Specification
Chemical Composition(API Spec 5CT / ISO 11960,N80 1)
|
Element |
PSL1 |
Note |
|
C |
≤ 0.43% |
Control the carbon content to balance strength and welding performance |
|
Mn |
≤ 1.60% |
Solid solution strengthening, improve strength |
|
P |
≤ 0.030% |
Harmful impurities, strictly controlled |
|
S |
≤ 0.030% |
Harmful impurities, strictly controlled |
|
Si |
≤ 0.45% |
Deoxidizer, improve strength |
|
CEIIW |
No mandatory requirements |
ERW products can be arranged according to the agreement |
Physical Properties
|
Property |
Value/Range |
Test Conditions |
|
Density |
≈ 7.85 g/cm³ |
Room Temperature (20°C) |
|
Melting Point |
≈ 1420–1460℃ |
--- |
|
Elastic modulus |
≈ 207 GPa |
Room Temperature |
|
Thermal Conductivity |
≈ 50 W/(m·K) |
Room Temperature |
|
Coefficient of Thermal Expansion (20-100°C) |
≈ 11.5 × 10⁻⁶ /K |
--- |
|
Poisson's ratio |
≈ 0.28 |
Room Temperature |
Mechanical Properties (Typical value,N80 1)
|
Performance |
PSL1 |
Implementation standards |
|
Minimum Yield Strength |
552 MPa |
API Spec 5CT / ISO 11960 |
|
Maximum Yield Strength |
758 MPa |
API Spec 5CT / ISO 11960 |
|
Minimum Tensile Strength |
689 MPa |
API Spec 5CT / ISO 11960 |
|
Maximum Tensile Strength |
- |
API Spec 5CT / ISO 11960 |
|
Elongation |
Calculate and determine using the tabular formula from API Spec 5CT |
API Spec 5CT |
Note: The 'N80-1' in API 5CT N80-1 indicates a minimum yield strength of 80,000 psi (approximately 552 MPa), with the number representing thousands of pounds per square inch (ksi). The actual yield strength of the pipe typically ranges from 552 to 758 MPa, and the tensile strength ranges from 689 to 760 MPa.
Applicable Media
1. Petroleum, Natural Gas:
Medium-deep and Deep Well Tubing, Casing and Couplings (Non-H₂S Sweet Wells)
2. High-pressure oil and gas wells:
Conventional non-sulfur, moderately CO₂-containing medium-deep and deep oil and gas wells
3. General Fluids:
Well Completion and Oil Production Operations for Sulfur-Free Oil and Gas Wells
Note: API 5CT N80-1 is not suitable for H₂S-containing acidic oil and gas conditions; for H₂S-containing conditions, API 5CT sour-resistant steel grades L80-1, C90, T95 or corrosion-resistant alloys 13Cr and 22Cr should be selected.
Product Form and Manufacturing Process
Seamless steel pipe (Seamless)
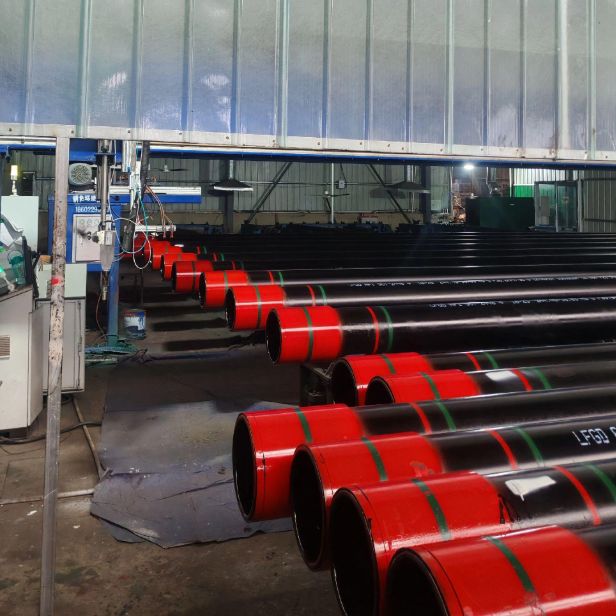
• Process: Hot Rolling Poking + Extension Rolling + Normalizing / Normalizing + Tempering Heat Treatment
• Outer Diameter Range: 114.3–508 mm (4-1/2"–20")
• Wall thickness range: 5.21–16.13 mm
• Features: Seamless, with high pressure-bearing strength; suitable for medium-deep and deep high-pressure non-sulfur oil and gas wells
• Typical applications: Medium-deep wells, deep well downhole tubing and casing; downhole wellhead connection components
Straight Seam High-Frequency Resistance Welded Pipe (ERW)
• Process: Hot-rolled coil → Cold bending forming → High-frequency resistance welding → Normalizing heat treatment
• Outer Diameter Range: Typically ≤ 508 mm (20\")
• Wall thickness range: Typically ≤ 16 mm
• Features: High dimensional accuracy, high production efficiency, and significant cost advantages
• Typical applications: Medium-deep wells, deep wells, high-pressure, and sulfur-free oil and gas wells
• Welding Heat Input Control: The high-frequency welding process ensures that the weld seam meets all API 5CT requirements for ERW products.
Applicable Standards and Delivery Condition
• Standard: API Spec 5CT,ISO 11960,GB/T 19830
• Product Specification Level: Default to PSL1 (Basic Level); PSL2 is an annexed upgrade in Annex H, which requires explicit agreement in the contract to enable.
• Delivery Status: Normalizing / Normalizing + Tempering
• End Processing: Flat Ends, Beveled Ends, Threaded Ends (STC, LTC, BTC), Premium Special Fitting Ends
• Certificate:Provide material certificates in accordance with the procurement contract requirements; PSL1 does not have mandatory SR15 certificates and full-process traceability mandatory clauses. Upon activation of Annex H (PSL2), SR15.1 and SR15.2 become mandatory.
Heat Treatment System and Welding Key Points
The final performance of API 5CT N80-1 depends on the hot rolling, normalizing, or quenching and tempering heat treatment processes:
1. Controlled rolling and controlled cooling or quenching and tempering
N80-1(Conventional):
Heat to 1100–1200°C for rough rolling, controlled rolling in the 850–950°C finishing temperature range, followed by controlled cooling within 600–800°C. A uniform ferrite + pearlite microstructure is obtained.
N80-1Q (Quenched and Tempered):
Austenitize by heating to 850–950°C, followed by water quenching or oil quenching, then temper at 550–650°C with a holding time of 1–2 hours. A uniform tempered martensite microstructure is obtained, ensuring a balanced combination of strength and toughness.
2. Post-weld heat treatment (if required)
If stress relief is required after pipe ring weld welding, post-weld heat treatment at 550–650°C for 1–2 hours can be performed. Post-weld heat treatment should pay attention to controlling the heating and cooling rates to avoid affecting the microstructure and properties of the base material.
Important Reminder:
• In conventional oil and gas transmission environments without H₂S, stress relief heat treatment is typically not required after welding.
• In acidic environments containing H₂S, N80-1 is not recommended for use in pipelines; instead, sulfide-resistant steel grades (L80, C90, T95) should be selected.
• During welding, strict control of heat input and interpass temperature is required to prevent grain coarsening in the heat-affected zone and excessive hardness.
API 5CT N80-1 is suitable for oil tubes, casing, and couplings in medium to deep wells, and is recommended for the following range:
Application Fields
-
Oil and Natural Gas Drilling
• Medium-deep well oil pipes and casing
• High-pressure oil and gas wells
• Conventional oil and gas well completion and production operations
• Wellhead equipment and gathering and transportation pipelines -
Urban gas
• Medium and low pressure gas pipeline network
• Gas pressure regulating station inlet and outlet pipelines -
Water Conveyance and Irrigation Engineering
• Medium and low pressure water transmission main pipeline
• Large-scale water conservancy project supporting pipelines -
Structural piping
• General structural support
• Building steel structure support pipe
Delivery and Customization
We offer flexible and reliable supply chain solutions to ensure you receive API 5CT N80-1 oil casing that perfectly matches your project requirements.
Customizable Material Forms
We support producing various basic and special shapes according to drawings or specifications.
|
Form |
Seamless Pipe
|
Straight Seam Electric Resistance Welded Pipe (ERW)
|
|---|---|---|
|
Conventional Range |
Outer diameter: 114.3–508 mm; Wall thickness: 5.21–16.13 mm |
Outer diameter: 114.3–508 mm; Wall thickness: 5.21–16.13 mm |
|
Customization Capability |
Hot-rolled seamless pipes, fixed-length cutting, bevel processing, pipe end threads, special heat treatment conditions |
High-frequency straight-seam welded pipes, fixed-length cutting, bevel processing, galvanization/plastic coating treatment |
Why Choose Us? - Reliable Engineering Technology. Dependable Delivery.
We are not just a supplier, but a trusted materials partner for you in China.

Vertically Integrated Production
Own 20,000㎡ facility with 10+ automated lines (8,000+ tons/year). In-house tooling & die center enables rapid customization and effective cost control - no middleman markup.
Strict Quality Control at Every Stage
Full traceability across key QC checkpoints throughout production. 100% compliant with ASTM/ASME, EN, and GB standards. Material test reports available with every shipment.

Reliable Delivery & Export Packaging
10+ years exporting to Europe, North America, Southeast Asia & Middle East with waterproof and anti-rust protection, combined with flexible shipping options ensures safe and on-time arrival.
Sample Validation Before Mass Production
We provide free samples for quality verification, allowing you to place bulk orders only after approval. We ensure consistency from sample to mass production by accurate dimensional measurement and transparent manufacturing.
Summary of Core Advantages
Matching medium to high strength with good toughness
Minimum yield strength of 552 MPa, minimum tensile strength of 689 MPa, along with good impact toughness, making it suitable for medium-deep well and high-pressure well environments.
Good welding performance
Designed with a moderate carbon equivalent (CEIIW ≤ 0.45), it exhibits excellent field ring weld construction performance. The weld heat-affected zone has good toughness and resistance to cold cracking.
High Cost-Performance
N80-1 is the main grade of medium-to-high strength level in API 5CT. It offers moderate strength and economical cost, making it an efficient and cost-effective choice for conventional oil and gas wells.
Diverse product forms
Covers various manufacturing processes such as seamless tubes and ERW, with an outer diameter range of 114.3–508 mm.
Divided into two types
N80-1and N80-1Q. N80-1 is conventional hot-rolled/normalized, and N80-1Q is quenched and tempered. It can be selected according to operating conditions.
Compliant with multiple international standards
API Spec 5CT, ISO 11960, GB/T 19830, etc.
FAQ
Q: What is the difference between API 5CT N80-1 PSL1 and PSL2? How to choose between them?
Q: What are the differences between API 5CT J55, K55, N80-1, L80-1, and P110? How to choose?
Q: What is the maximum operating temperature for API 5CT N80-1?
Q: What is the welding performance of API 5CT N80-1?
Q: How is the corrosion resistance of API 5CT N80-1?
Q: Can API 5CT N80-1 replace ASTM A53 or J55?
Hot Tags: api 5ct n80-1, China api 5ct n80-1 manufacturers, suppliers, factory