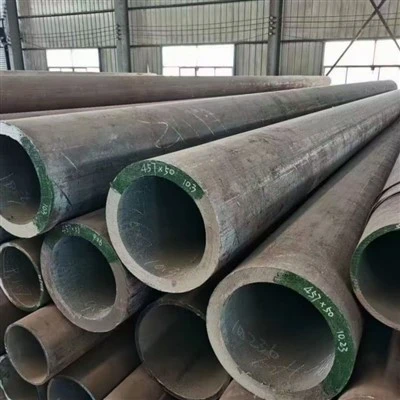
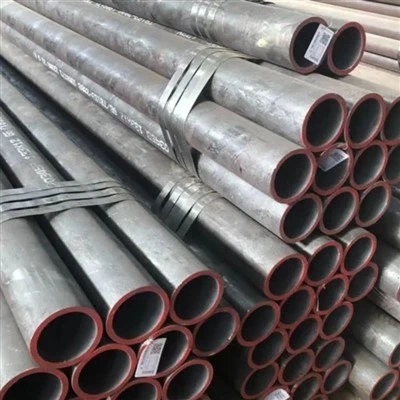
Products Features

Excellent high-temperature oxidation and corrosion resistance (core advantage)
The core advantage of ASTM A335 P9 lies in its excellent high-temperature oxidation resistance and corrosion resistance. Thanks to the addition of 8-10% chromium (Cr), P9 can form a dense Cr₂O₃ oxide film at high temperatures, effectively resisting high-temperature oxidation and thermal corrosion. Its upper limit for oxidation resistance reaches 550-600°C, which is significantly higher than that of P1 (≤450°C) and P11 (≤538°C), and comparable to P5. In high-temperature sulfur-containing environments typical of refineries, P9 exhibits superior corrosion resistance compared to low-chromium grades, effectively withstanding high-temperature sulfidation corrosion and combined oxidation-sulfidation corrosion. Additionally, its 1% molybdenum content, higher than P5's 0.5% Mo, further enhances its high-temperature creep resistance. While its minimum tensile strength is 415 MPa and minimum yield strength is 205 MPa-placing it on par with P5-in terms of high-temperature oxidation resistance and creep resistance, P9 offers distinct advantages.

Excellent high-temperature strength and creep resistance
ASTM A335 P9 maintains good strength levels at high temperatures. Thanks to the addition of 1% molybdenum (Mo) (higher than the 0.5% Mo in P5) and higher chromium content, P9 exhibits superior high-temperature creep rupture strength compared to P5 in the temperature range of 500-600°C. Under conditions at 550°C, P9 offers better oxidation resistance and high-temperature strength than P5, making it suitable for high-temperature and high-pressure piping systems operating at higher temperature and pressure grades. While its high-temperature strength retention is comparable to P5, P9 has superior creep resistance, allowing for long-term service in more severe high-temperature and high-pressure environments.

Good machinability and formability
ASTM A335 P9 exhibits good cold and hot working properties, allowing for various forming processes such as hot bending, cold bending, and forging. With a moderate alloy content, it demonstrates excellent formability during cold bending, making it suitable for manufacturing pipe fittings like elbows, tees, and reducers. It should be noted that due to its higher chromium content (8-10%), P9 has a slightly greater tendency for work hardening compared to P5. Therefore, it is recommended to include appropriate intermediate annealing steps during forming processes. Its machinability is comparable to that of P5, and conventional machining methods can be employed for processing.

Good welding performance and strict post-weld heat treatment requirements
ASTM A335 P9 exhibits good weldability. However, due to its higher chromium content (8-10%), it has a greater tendency for hardening in the heat-affected zone compared to P5, thus requiring stricter welding procedures and post-weld heat treatment (PWHT). It is recommended to preheat before welding at 200-300°C. After welding, PWHT must be performed by heating to 730-780°C, holding at temperature, and then cooling slowly. This process helps eliminate residual welding stresses, soften the heat-affected zone, and ensure the toughness and crack resistance of the welded joint.
Good organizational stability and long-term service reliability
ASTM A335 P9 exhibits good organizational stability when in long-term service at temperatures ≤600℃. Its higher chromium content (8-10%) effectively enhances the material's oxidation resistance and high-temperature corrosion resistance. The addition of 1% Mo further improves high-temperature creep strength, ensuring organizational stability during prolonged high-temperature service. After normalization and tempering (N+T) heat treatment, P9 obtains a uniform and fine ferrite + carbide microstructure, guaranteeing organizational stability and reliability under high-temperature service conditions.
Technical Specifications
Chemical Composition(ASTM A335 / ASME SA335)
|
Element |
Standard requirements |
Note |
|
C |
≤ 0.15% |
Low-carbon design ensures weldability and toughness |
|
Mn |
0.30 - 0.60% |
Solid solution strengthening, improve strength |
|
P |
≤ 0.025% |
Harmful elements, strictly controlled |
|
S |
≤ 0.025% |
Harmful elements, strictly controlled |
|
Si |
0.25 - 1.00% |
Deoxidizer, improve high-temperature oxidation resistance |
|
Cr |
8.00 - 10.00% |
Core elements that provide excellent high-temperature oxidation and corrosion resistance |
|
Mo |
0.90 - 1.10% |
Core elements to improve high-temperature creep fracture strength (content higher than P5) |
|
Fe |
Remaining quantity(≈ 89%) |
Matrix element |
Physical Properties
|
Performance |
Numerical Value/Range |
Test conditions |
|
Density |
≈ 7.75 g/cm³ |
Room Temperature (20°C) |
|
Melting Point |
≈ 1370-1420°C |
- |
|
Electrical resistance |
≈ 0.45 μΩ·m |
Room Temperature |
|
Thermal Conductivity |
≈ 32 W/(m·K) |
Room Temperature |
|
Coefficient of Thermal Expansion (20-100°C) |
≈ 11.2 × 10⁻⁶ /K |
- |
|
Elastic modulus (Young's modulus) |
≈ 200 GPa |
Room Temperature |
|
Poisson's ratio |
≈ 0.28 |
Room Temperature |
|
Magnetism |
Ferromagnetic |
Ferrite structure, which is magnetic |
Mechanical Properties (Normalized + Tempered, Typical Values, ASTM A335)
|
Performance |
Typical value |
Implementation standards |
|
Tensile Strength |
≥ 415 MPa |
ASTM A335 |
|
Yield Strength (0.2% Offset) |
≥ 205 MPa |
ASTM A335 |
|
Elongation (gauge length 2in/50mm) |
≥ 30% |
ASTM A335 |
|
Hardness |
≤ 217 HB (typical value) |
- |
Note: The strength level of P9 is the same as P5 (≥415 MPa). However, its core advantage lies in the excellent high-temperature oxidation resistance and corrosion resistance brought by 8-10% chromium content, as well as the superior creep resistance provided by 1% Mo, rather than enhanced strength. For higher strength or higher temperature grades, it is recommended to select P91.
High-temperature performance
ASTM A335 P9 maintains good strength levels at high temperatures and is suitable for long-term high-temperature service conditions up to 600°C:
|
Temperature |
Tensile strength (MPa, approximately) |
Performance retention rate |
|
Room temperature (20°C) |
≥ 415 |
100% |
|
400°C |
≈ 380 |
≥ 92% |
|
450°C |
≈ 350 |
≥ 84% |
|
500°C |
≈ 290 |
≥ 70% |
Long-term Thermal Stability and Microstructural Stability:
ASTM A335 P9 exhibits good microstructural stability during long-term service at temperatures ≤600°C. The addition of 8-10% Cr effectively enhances high-temperature oxidation resistance and thermal corrosion resistance, while the inclusion of 1% Mo further improves creep strength. However, microstructural stability decreases and oxidation resistance is reduced when used for extended periods above 620°C; thus, it is not recommended for long-term service above this temperature. For higher temperature grades, P91 or P92 is suggested.
Heat treatment system
The final performance of ASTM A335 P9 is highly dependent on the heat treatment regime, with common specifications as follows:
1. Normalizing Treatment (Normalizing)
Heat to 925-955°C, hold for a sufficient time (approximately 1 hour per inch of wall thickness), then air cool. This results in a uniform, fine-grained ferrite + carbide microstructure, preparing for subsequent tempering.
2. Tempering treatment(Tempering)
Heat to 730-780°C, hold for sufficient time, then air cool. This eliminates stresses induced by normalizing, optimizes toughness and plasticity, and achieves the final service properties.
3. Full Annealing (Optional)
Heat to 840-870°C, hold at temperature, then furnace cool to approximately 650°C, followed by air cooling to room temperature. This is used to eliminate cold working stresses or improve cold working formability.
Attention: Post-weld heat treatment (PWHT) must be performed after welding. It involves heating to 730-780°C, holding at temperature, and then slow cooling to eliminate residual welding stresses and soften the heat-affected zone.
Due to its higher chromium content (8-10%), P9 has a greater tendency to harden in the weld heat-affected zone compared to P5. It is recommended to strictly control welding heat input and preheating temperature (200-300°C).
The heat treatment temperature and time must be strictly controlled to avoid grain coarsening or performance fluctuations.
Applicable Media
High-temperature steam:
Main steam pipelines of power plants (≤600°C), boiler superheater tubes, reheater tubes
Petroleum refining media:
High-temperature sulfur-containing process pipelines for atmospheric and vacuum distillation, catalytic cracking, hydrotreating, delayed coking, etc.
High-temperature sulfur-containing media:
High-temperature sulfur-containing oil and gas media, acidic media environments in refineries
High-temperature process gases:
High-temperature and high-pressure pipelines of chemical facilities for ammonia synthesis, methanol production, etc.
High-temperature heat transfer media:
Heat transfer oil pipelines, high-temperature heat transfer systems
Note: ASTM A335 P9 is not suitable for strongly corrosive media such as strongly oxidizing acids (e.g., concentrated nitric acid) and high-temperature, high-concentration chlorides. Its upper oxidation temperature limit is approximately 600°C; P91 or P92 is recommended above this temperature. In high-temperature, high-pressure hydrogen-containing environments (e.g., hydroprocessing units), the risk of hydrogen corrosion should be assessed.
ASTM A335 P9 is suitable for high-temperature (500-600°C) service conditions involving sulfur-corrosive media. It is an important material selection for high-temperature process piping in the oil refining and petrochemical industries, recommended for use in the following areas:
Application Fields
-
Petroleum Refining (Core Application)
● High-temperature process pipelines for catalytic cracking units
● High-temperature and high-pressure pipelines for hydrotreating/hydrocracking units
● High-temperature pipelines of the atmospheric and vacuum distillation unit
● Delayed Coking Unit Process Piping
● Refinery heater tubes, heat exchanger tubes -
Petrochemical Engineering (Core Applications)
● High-temperature pipelines in ethylene cracking units
● Aromatics unit high-temperature process piping
● Petrochemical heating furnace tube system -
Fossil fuel power generation
● Main Steam Piping for Subcritical/Supercritical Power Plants (≤600°C)
● Superheater tubes, reheater tubes
● High-temperature steam pipeline system -
High-temperature and high-pressure pipe fittings
● High-temperature elbows, tees, and reducers
● Forged pipe fittings, flanges
Delivery and Customization
We offer flexible and reliable supply chain solutions to ensure you receive ASTM A335 P9 alloy steel pipes that perfectly match your project requirements.
Customizable material forms
We support producing various basic and special shapes according to drawings or specifications.
|
Form |
 Seamless Steel Pipe
|
 Large-diameter Thick-walled Pipe
|
 Alloy Steel Pipe
|
|---|---|---|---|
|
Conventional Range |
Outer Diameter: 10.3 - 1067 mm; Wall Thickness: 1 - 150 mm |
Outer Diameter: 219 - 1067 mm; Wall Thickness: 20 - 150 mm |
Outer Diameter: 10.3 - 610 mm; Wall Thickness: 1 - 50 mm |
|
Customization Capability |
Hot-rolled / cold-drawn seamless tubes, fixed-length cutting, bevel machining, pipe end threads, special heat treatment conditions (normalizing + tempering / annealing) |
Hot expansion, fixed-length cutting, bevel machining, special heat treatment conditions |
Cold-drawn precision tubes, fixed-length cutting, special surface treatment |
Why Choose Us? - Reliable Engineering Technology. Dependable Delivery.
We are not just a supplier, but a trusted materials partner for you in China.

Vertically Integrated Production
Own 20,000㎡ facility with 10+ automated lines (8,000+ tons/year). In-house tooling & die center enables rapid customization and effective cost control - no middleman markup.

Strict Quality Control at Every Stage
Full traceability across key QC checkpoints throughout production. 100% compliant with ASTM/ASME, EN, and GB standards. Material test reports available with every shipment.

Reliable Delivery & Export Packaging
10+ years exporting to Europe, North America, Southeast Asia & Middle East with waterproof and anti-rust protection, combined with flexible shipping options ensures safe and on-time arrival.

Sample Validation Before Mass Production
We provide free samples for quality verification, allowing you to place bulk orders only after approval. We ensure consistency from sample to mass production by accurate dimensional measurement and transparent manufacturing.
FAQ
Q: What are the main advantages of ASTM A335 P9?
Q: What is the difference between ASTM A335 P9 and P5? How to choose between them?
Q: What is the difference between ASTM A335 P9 and P11? How to choose between them?
Q: What is the maximum service temperature for ASTM A335 P9?
Q: What is the welding performance of ASTM A335 P9?
Q: What is the corrosion resistance of ASTM A335 P9?
Hot Tags: astm a335 p9, China astm a335 p9 manufacturers, suppliers, factory